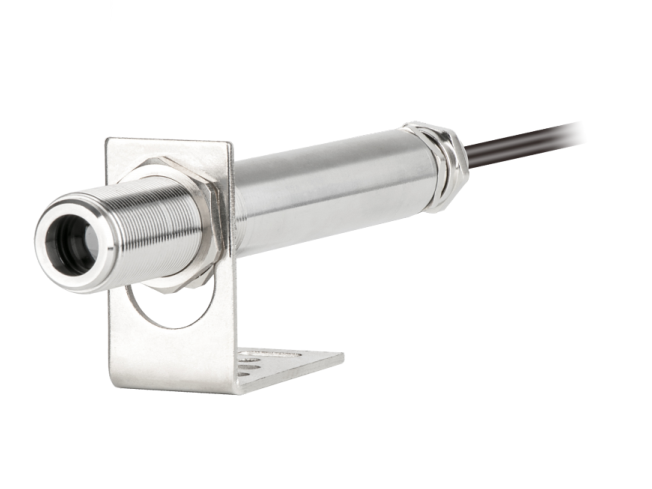
The CST-DL infrared temperature sensor is a non-contact pyrometer for hot objects up to 1400 °C, with an ultra-fast 40 ms response time, 4–20 mA analogue output and narrow 100:1 field of view. It is designed for hot metal billets, kilns, boilers and induction furnaces, and for hot-object detection in counting and positioning systems on production lines.
The IP65 stainless-steel housing operates reliably in dusty, humid and hot industrial environments. Equipment Industrial Solution Co., Ltd (ISE) supplies the CST-DL and advises on range, field of view and mounting position.
Advantages of the CST-DL infrared pyrometer
- Measures up to 1400 °C without touching the target – no probe wear or burn-out like thermocouples.
- Ultra-fast 40 ms response – keeps up with fast-moving hot material on conveyors and rolling lines.
- Narrow 100:1 field of view (50:1 optional) – accurate aiming at small or distant targets.
- 4–20 mA output for direct connection to PLCs, indicators and temperature controllers.
- Accuracy 0.75 % of reading, repeatability 0.3 %.
- IP65 stainless-steel housing for harsh environments.
CST-DL infrared temperature sensor specifications
| Parameter | Value |
|---|---|
| Model | CST-DL |
| Temperature range | 0 °C to 500 °C; 500 °C to 1400 °C |
| Spectral response | 1.0 µm |
| Accuracy | 0.75 % of reading |
| Repeatability | 0.3 % of reading |
| Response time (t₉₀) | 40 ms |
| Emissivity | 1.00 (fixed) |
| Field of view (distance : spot) | 50:1, 100:1 |
| Output | 4–20 mA |
| Power supply | 24 VDC ±15 %, 50 mA |
| Housing / protection | Stainless steel, IP65 |
Non-contact temperature measurement applications
- Boilers and combustion chambers: continuous flame and wall temperature for combustion optimisation and early fault detection.
- Metallurgy and metalworking: billets, plates and bars during rolling, forging, casting and heat treatment.
- Induction furnaces: real-time temperature feedback for induction heating and hardening.
- Glass production: molten glass, forming and annealing.
- Kilns and dryers: surface and process temperature where contact sensors cannot be installed.
- Plastics and rubber (extrusion, moulding, curing), food processing and automotive (welds, brakes, exhausts).
- Counting and positioning hot objects on conveyors.
- Predictive maintenance: detecting hot spots on machinery, bearings and electrical equipment.
Selection and installation tips
- A 100:1 field of view means a spot of about 10 mm at 1 m. The target must be larger than the spot.
- Emissivity is fixed at 1.00; for shiny, low-emissivity metals, apply an offset against the actual temperature or aim at an oxidised area.
- Avoid dense smoke, steam and dust in the line of sight; use a sighting tube or air purge in combustion chambers.
- Choose the right range: 500–1400 °C for red-hot metal and kilns; the lower range for moderate temperatures.
FAQ
How does an infrared temperature sensor differ from a thermocouple?
A thermocouple must touch the target, so it is slower and wears out at high temperature. An infrared sensor measures remotely with 40 ms response, no wear, and can measure moving objects.
Is the CST-DL a handheld IR gun?
No. The CST-DL is a fixed-mount sensor with 4–20 mA output for continuous monitoring and control on production lines.
Related products
Where to buy the CST-DL infrared temperature sensor?
EQUIPMENT INDUSTRIAL SOLUTION CO., LTD (ISE) – Ho Chi Minh City, Vietnam – supplies genuine the CST-DL infrared temperature sensor with technical consulting, fast quotation and on-site commissioning support across Vietnam and Southeast Asia.
Contact us: Sales +84 909 617 185 – Technical +84 979 117 185 – Email: [email protected]